Three-Axis Laser Welding Machine: Working Principle, Applications And Selection Guide
Release time:2026-09-18
Visits:4
A three-axis laser welding machine moves a laser head along X, Y and Z to join sheet metal and small-to-mid-size parts at speed, with repeatable weld quality. It fills the gap between a handheld laser welder and a six-axis welding robot. For many production shops it is the more practical option: it costs less, takes less floor space, and is far easier to program. This article explains how these machines work, where they make sense, and what to check before you buy one.
What Is a Three-Axis Laser Welding Machine?
The name refers to the motion system. The machine carries a laser welding head on three linear axes. X and Y position the head across the work area, while Z raises and lowers it to set the focal height. The rest of the system is the laser source, the welding head with its focusing optics, a CNC controller, and a shielding gas supply.
Two frame designs are common. In a gantry machine, the head travels on a bridge over a fixed table, which suits large flat panels. In a moving-table design, the head stays put while the table feeds the part underneath, which suits smaller parts and heavier fixtures. Both give the head access to any point inside a rectangular working envelope, with the beam held vertical or at one fixed angle.
That last point is what separates a three-axis machine from a robot. A robot swivels its wrist to follow curved seams in three dimensions. A three-axis machine welds flat and gently curved joints that sit in a single plane. For work that fits that description, the simpler machine is usually enough.
How the Welding Happens
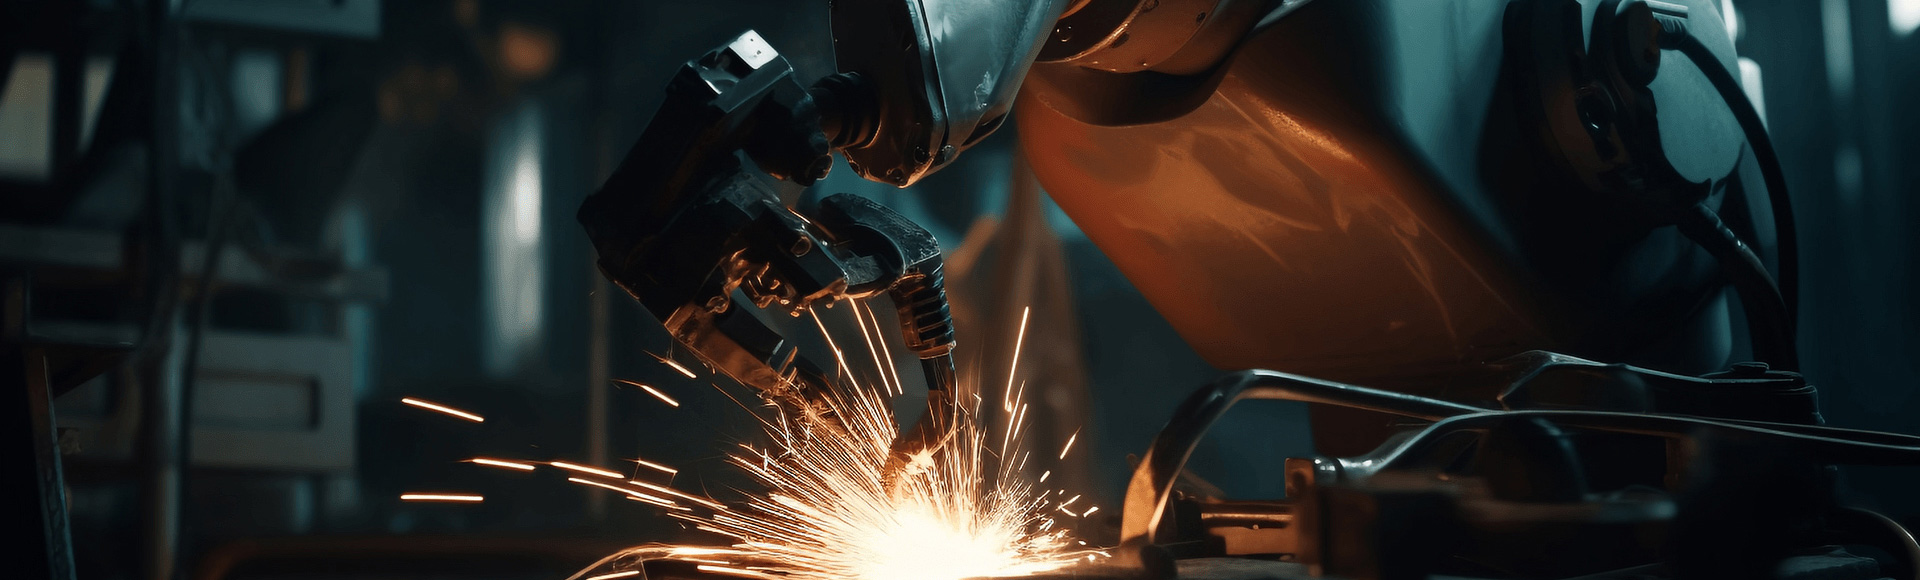
The laser beam passes through focusing optics and lands on the joint as a small, intense spot. The metal absorbs the energy and melts, forming a weld pool that travels with the head. Two modes occur in practice. Conduction mode, with a larger spot and lower power density, melts a shallow, wide bead and suits thin sheet. Keyhole mode, with a tighter spot, vaporizes a channel in the metal that lets the beam reach deep into the joint. Keyhole welding gives deep penetration and a narrow heat-affected zone, which is why laser welding beats MIG on distortion-sensitive parts.
Shielding gas, usually argon for steel and argon-helium mixes for aluminum, protects the hot pool from oxidation. Focal position, travel speed and power interact: push power up or slow the head down and penetration grows, but so does the risk of burn-through on thin material.
Three-Axis Machine or Welding Robot?
Match the machine to the joint geometry:
A three-axis laser welding machine fits flat panels, enclosures, trays, tanks, frame parts and other parts with straight or mildly curved seams. It also handles high-volume work where repeatability matters more than flexibility.
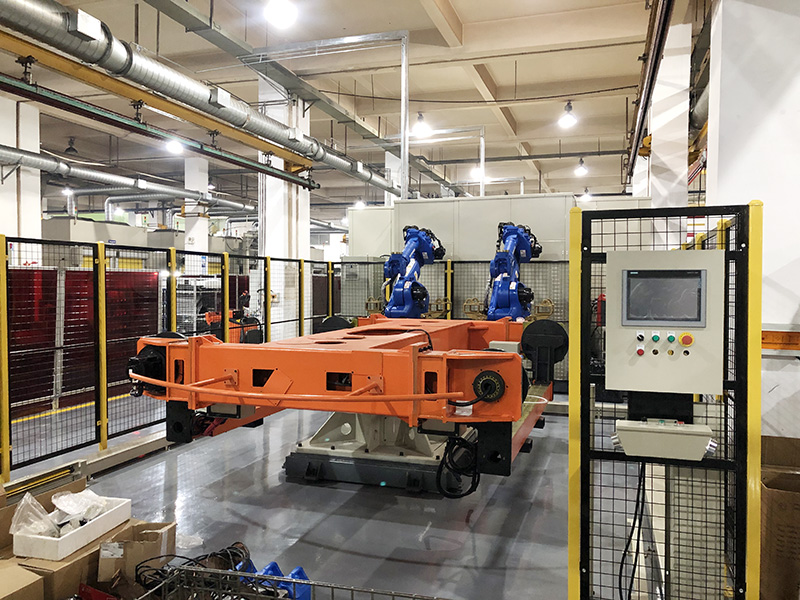
A welding robot fits parts with curved 3D seams, deep pockets, or several different joint orientations in one product. It adds reach and wrist motion, at higher cost and with more complex programming.
A rotary positioner extends a three-axis machine to cylindrical work such as filter housings, motor cases and small pressure vessels. The part rotates under the head while the axes handle length and height.
Typical Applications
Three-axis laser welding is common in sheet metal fabrication: control cabinets, enclosures, battery cases and trays, chassis brackets, heat shields, small tanks and tubular frames. Automotive suppliers use it for brackets and housings that used to go to MIG, gaining speed and less post-weld grinding. Switchgear and electrical equipment makers weld contacts and housings where heat input has to stay low.
How to Choose a Three-Axis Laser Welding Machine
Work through these points before ordering:
Laser power. 1 kW handles thin sheet up to roughly 2-3 mm of steel. 1.5-3 kW extends penetration to 6-8 mm and lifts productivity on aluminum. Match power to the thickest material in your mix, not the average.
Working envelope. Table size should cover your largest part with room for fixtures. A machine that is too small becomes the bottleneck as soon as one part grows.
Control system. Look for easy programming, saved weld recipes, and the option of seam tracking or height sensing if your parts vary.
Rotary axis. If round parts are in your future, buy the machine with the positioner interface from day one.
Safety enclosure. Laser welding is a Class 1 laser hazard when enclosed properly. A certified enclosure with interlocks protects operators and keeps audits simple.
Maintenance and Safety
Keep the optics clean, check nozzle and shielding gas flow, and watch the water cooling circuit that protects the laser source. Weld fume extraction matters too, since laser welding produces fine fume. Operator training should cover the interlock system before it covers the welding program.
Bottom Line
If your parts are flat or near-flat and the seams repeat, a
three-axis laser welding machine will likely pay for itself faster than a robot cell, and it will hold weld quality shift after shift. Dade Heavy Industry builds three-axis and robotic laser welding equipment, including 3D laser welding workstations, and can size a machine around your actual parts and cycle times.